Industrial Food Ingredient Solutions

Benefits of Freeze Drying

Unlocking superior nutrition, ambient stability, and operational efficiency for global food manufacturers.

Freeze-Dried Technology: Uncompromising Quality You Can Count On

When evaluated across product consistency, sensory authenticity, nutritional retention, and long-term economic value, freeze-dried fruits, vegetables, and dairy solutions represent the benchmark choice for industrial food manufacturers and brand owners worldwide.

By utilizing low-temperature vacuum sublimation (lyophilization), freeze-drying gently removes moisture while leaving the delicate cellular structure of raw ingredients completely intact. This process effectively locks in vibrant natural colors, intense aromas, essential bio-actives, and authentic flavors, delivering clean-label ingredients that meet stringent global food processing standards.

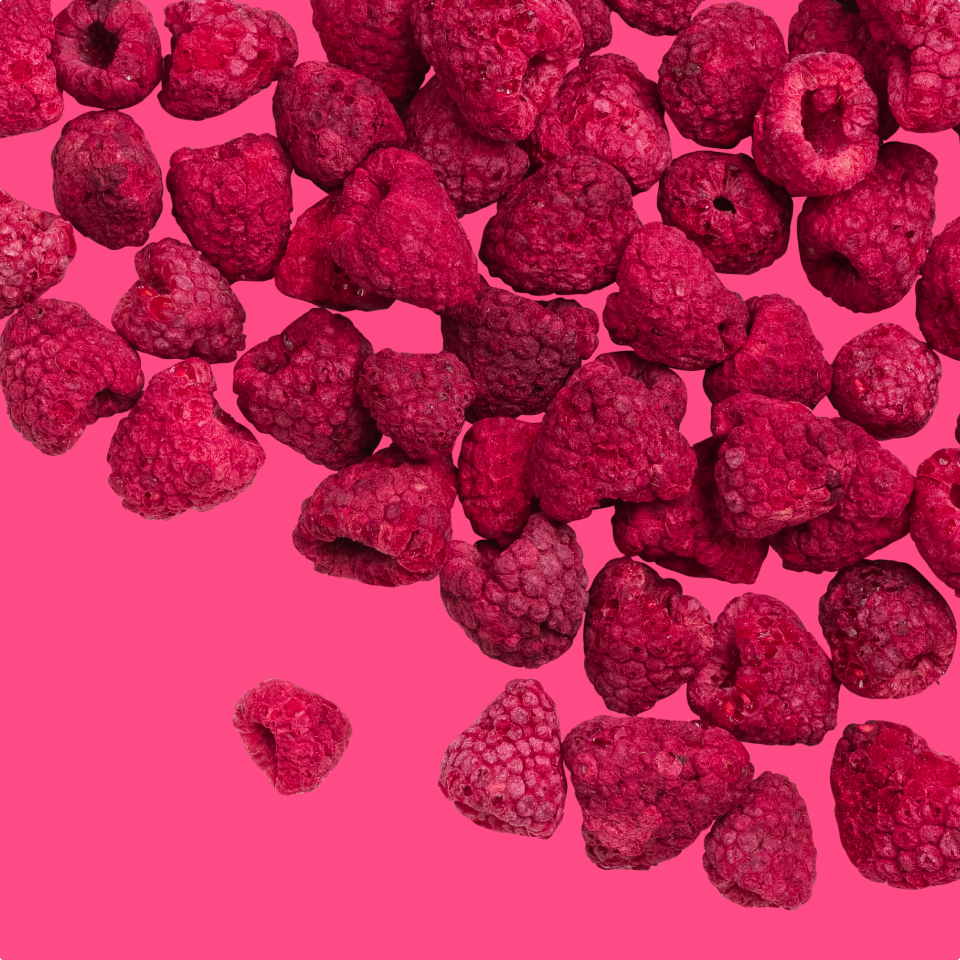
Premium BRC-certified freeze-dried raspberries for B2B food manufacturing

Key Industrial Benefits of Freeze-Drying Technology

Designed to solve complex technical challenges faced by research and development engineers, food technologists, and international procurement managers.

01

Maximum Nutritional & Vitamin Retention

Unlike traditional thermal drying methods (such as air drying or spray drying) that degrade heat-sensitive compounds, freeze-drying retains up to 97% of natural antioxidants, vitamins (including Vitamin C and A), fiber, and minerals. This enables food manufacturers to deliver authentic nutritional claims and clean-label appeal in health-conscious market sectors.
02

Peak Harvest Freshness & Sensory Fidelity

Raw materials are harvested at peak ripeness and immediately flash-frozen before processing. Sublimation preserves the internal structure, color, shape, and taste of fresh produce. Rehydration properties are instantaneous, delivering authentic crispiness, rich aromatic profiles, and visual impact in finished applications.

03

Supply Chain & Logistics Cost Optimization

Removing up to 98% of water content drastically reduces shipping weight while eliminating the requirement for expensive cold-chain logistics during transit and warehousing. Ambient storage stability minimizes storage overheads, optimizes freight container utilization, and insulates food manufacturers from seasonal price volatility.

04

Reduction of Commercial Food Waste

With an extended ambient shelf life exceeding 24 months in sealed barrier packaging, freeze-dried ingredients drastically reduce factory spoilage, shrinkage, and batch waste. Precise moisture control minimizes microbial activity and enzymatic breakdown without requiring synthetic preservatives or sulfur additions.

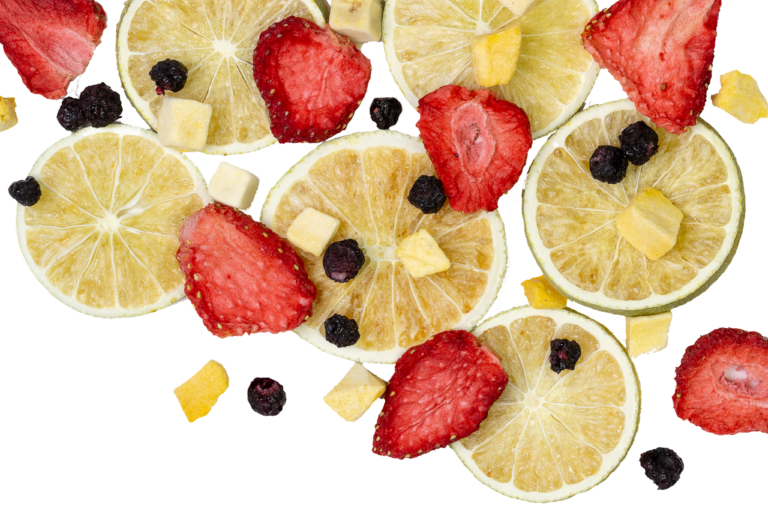
Assorted freeze-dried fruit pieces and powders for commercial baking and beverages

Versatile Formulations Across Global Food Sectors

Chaucer Foods provides customized slice sizes, dices, granules, and fine micro-powders tailored to specific industrial processing environments:

  • Breakfast Cereals & Granola: Maintains structural integrity and prevents sogginess in milk applications.
  • Confectionery & Chocolate: Zero water activity prevents sugar bloom and oil migration while providing vibrant contrast.
  • Functional Beverages & Smoothies: High solubility powders deliver intense color and natural fruit flavor profiles instantly.
  • Dairy & Ice Cream: Low moisture levels prevent ice crystal formation and texturizing anomalies in frozen matrixes.
  • Toddler Nutrition & Healthy Snacks: Easily melt-in-mouth textures free from added sugars, colorants, or synthetic additives.

Enterprise Manufacturing Specifications

Low Water Activity (Aw)

Typically Aw < 0.3, ensuring high microbiological stability and prolonged shelf-life under ambient storage environments.

Custom Particle Sizing

Available in whole fruits, precise dices (1mm to 10mm), crushed flakes, and ultra-fine mesh powders for seamless automation.

Certified Quality Control

Fully compliant with BRCGS, ISO 22000, Kosher, Halal, Non-GMO, and FDA global manufacturing standards.

Request Technical Datasheets & Product Samples

Explore our full specification catalog or speak directly with our food technologists to formulate custom ingredient solutions.

Get Catalog