High-Capacity Food Processing Engineered for Global Brands
At Chaucer Foods, our multi-continental production footprint enables leading multinational food manufacturers, retail brands, and foodservice distributors to access flexible, consistent, and secure supply chains. Backed by over 50 years of technical expertise, our facilities operate under strict international food safety protocols to deliver custom ingredients engineered for performance.
Industrial Freeze-Drying Processing
Operating one of the world's largest freeze-drying infrastructures, we utilize advanced vacuum sublimation technology to preserve 98% of natural nutrients, vibrant colors, and authentic flavor profiles without chemical additives or preservatives.
- Bulk Freeze-Dried Fruits (Dices, Whole, Slices & Granules)
- Concentrated Vegetable Powders & Micro-Porous Melts
- Real Dairy & Gourmet Freeze-Dried Cheese Inclusions
- Custom Moisture Barriers & Protective Coating Technologies
Precision Commercial Baking Lines
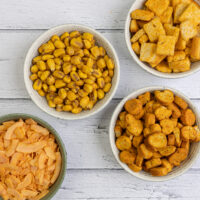
Our European specialized bakeries harmonize artisanal baking methods with automated batch control to produce consistent, high-crunch toppings, croutons, and baked inclusions engineered for long shelf-life integrity.
- Artisanal & Rustic Soup Croutons (Custom Granular Sizing)
- Seasoned Ciabatta Crumbs & Salad Toppers
- Gourmet Baked Bruschetta & Snack Dippers
- Low-Oil, Clean-Label Baking Formulations
Advanced Sublimation & Sizing Technology
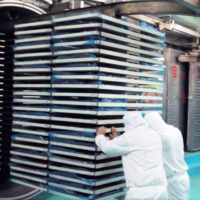
Our freeze-drying facilities house state-of-the-art continuous freeze-dryers with automated tray loader lines. Raw agricultural products undergo immediate blast freezing at peak harvest to lock in cellular structure before controlled low-pressure sublimation.
Post-drying processing includes high-precision optical sorting, metal detection, and custom milling capabilities—allowing us to meet precise particle sizes, screen specs, and density metrics required for automated food processing plants.
Automated Baking & Moisture-Control Baking
Our purpose-built baking facilities feature computer-controlled dough mixing, multi-stage proofing ovens, and precision slicing machines. By monitoring humidity levels and thermal profiles in real-time, we ensure absolute consistency in color, texture, and structural integrity.
Each batch undergoes rigorous moisture analysis to ensure minimal water activity (Aw), extending product shelf life in retail packaging and preventing moisture migration when used in complex food applications.
Strict Quality Compliance for Global Wholesale Procurement
Maintaining the absolute highest standard of food safety is central to our operational philosophy. Our global manufacturing facilities are audited by international bodies and strictly adhere to GFSI standards, providing procurement teams complete peace of mind.
International Food Safety Certifications
Every Chaucer production center operates under rigorous quality control frameworks, holding top-grade accreditations including BRCGS, ISO 22000, HACCP, Halal, Kosher, and Sedex SMETA social responsibility standards.
Custom OEM & Industrial Packaging Options
We supply flexible packaging solutions tailored for industrial buyers, including nitrogen-flushed bulk foil bags, heavy-duty corrugated cartons, tote bins, and retail-ready private label packs designed for maximum freshness retention.