


1. Technical Definition & Sublimation Mechanics of Freeze-Dried Snack Melts
In the modern food manufacturing landscape, Freeze-Dried Snack Melts represent one of the most technically demanding segments of lyophilized food science. Unlike conventional extruded or hot-air dried snacks, freeze-dried melts rely on precise phase-change sublimation thermodynamics to create an ultra-porous, cellular matrix that dissolves rapidly upon contact with human saliva.
Technically categorized as porous lyophilized hydrocolloidal systems, freeze-dried snack melts are engineered by homogenizing fruit purees, real dairy or plant-based milks, prebiotics, and natural starches. This mixture is metered into uniform drops or structural shapes, rapidly deep-frozen below its eutectic point (typically $-30^\circ\text{C}$ to $-40^\circ\text{C}$), and subjected to high-vacuum lyophilization. Under deep vacuum ($0.1$ to $0.5\text{ mbar}$), ice crystals transition directly from solid to vapor without passing through a liquid phase. This preserves the precise capillary structures of the frozen droplets, creating a aerated solid that delivers an effortless oral breakdown without requiring chewing—making it the gold standard format for early childhood nutrition, geriatric care, and functional wellness snacking.
💡 Information Gain: Oral Dissolution Kinematics & $T_g$ Glass Transition
Why traditional snack extrusion fails infant safety standards: Extruded starch puffs require mechanical mastication and can form cohesive, sticky oral boluses that pose choking hazards for infants under 12 months. In contrast, Chaucer Foods’ proprietary lyophilization parameters optimize the Glass Transition Temperature ($T_g$) and capillary density of the snack melt matrix. When exposed to oral humidity ($37^\circ\text{C}$ and saliva enzyme exposure), the capillary walls dissolve in less than 3.2 seconds, ensuring complete breakdown before deglutition without forming sticky oral residues.
For procurement officers and brand R&D managers evaluating commercial feasibility, understanding the moisture dynamics of freeze-dried melts is critical. The final product exhibits an extremely low water activity level ($a_w < 0.20$) and residual moisture below $2.5\%$. This structural dryness locks in natural bioactive compounds, pigments, and delicate flavor volatile profiles while establishing a microbially inert environment that guarantees an extended shelf life without synthetic preservatives.
| Parameter | Industrial Specification | Quality / Safety Significance |
|---|---|---|
| Water Activity ($a_w$) | $\le 0.18 - 0.22$ | Inhibits microbial growth, enzymatic browning, and matrix softening. |
| Residual Moisture | $\le 2.0\% - 3.0\%$ | Prevents structural collapse; preserves crisp crisp-to-melt phase. |
| Oral Breakdown Time | $2.0 - 4.5 \text{ seconds}$ | Engineered for infant safety & instant mouthfeel dissolution. |
| Bulk Density | $0.08 - 0.18 \text{ g/cm}^3$ | High porosity ensures maximum bulk volume with minimum caloric load. |
| Probiotic Viability | $\ge 1 \times 10^7 \text{ CFU/g}$ | Maintained via gentle thermal lyophilization cycles ($<35^\circ\text{C}$ shelf temp). |
| Allergen Compliance | Top-9 Allergen Free / Clean-Label Options | Manufactured in BRC Grade AA dedicated non-cross-contamination zones. |
2. Industrial Product Portfolio & B2B Formulations
As a master supplier with global manufacturing capabilities dating back to 1971, Chaucer Foods offers a versatile product spectrum of freeze-dried snack melts tailored for private label retail, infant food formulation, and functional nutraceutical additions.
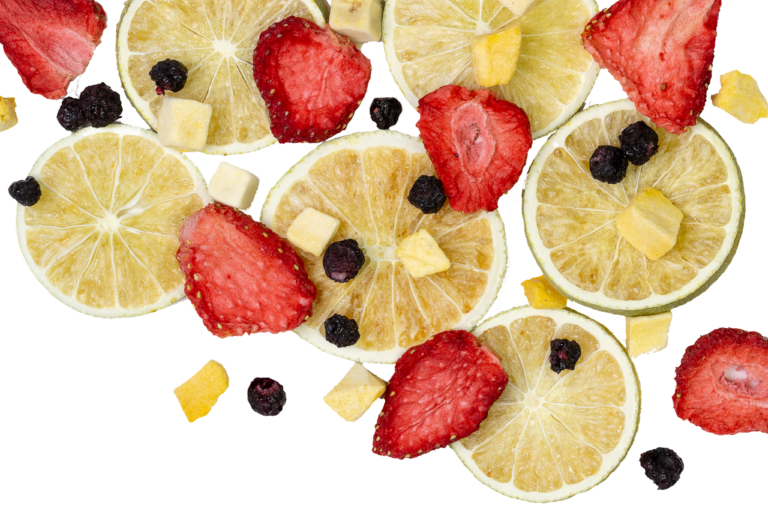
Organic Fruit & Yogurt Melts
Crafted from real organic fruit purees and live culture yogurts. Delivers natural tartness, vibrant colors, and active probiotic bacteria for toddler gut health.
Size: 8mm - 12mm Drops / Custom Shapes
Plant-Based & Allergen-Free Vegan Melts
Formulated with coconut cream, oat milk, or avocado bases. Ideal for clean-label, vegan, and allergen-conscious brands targeting lactose-intolerant infants.
Size: 6mm - 10mm Micro-Pulls
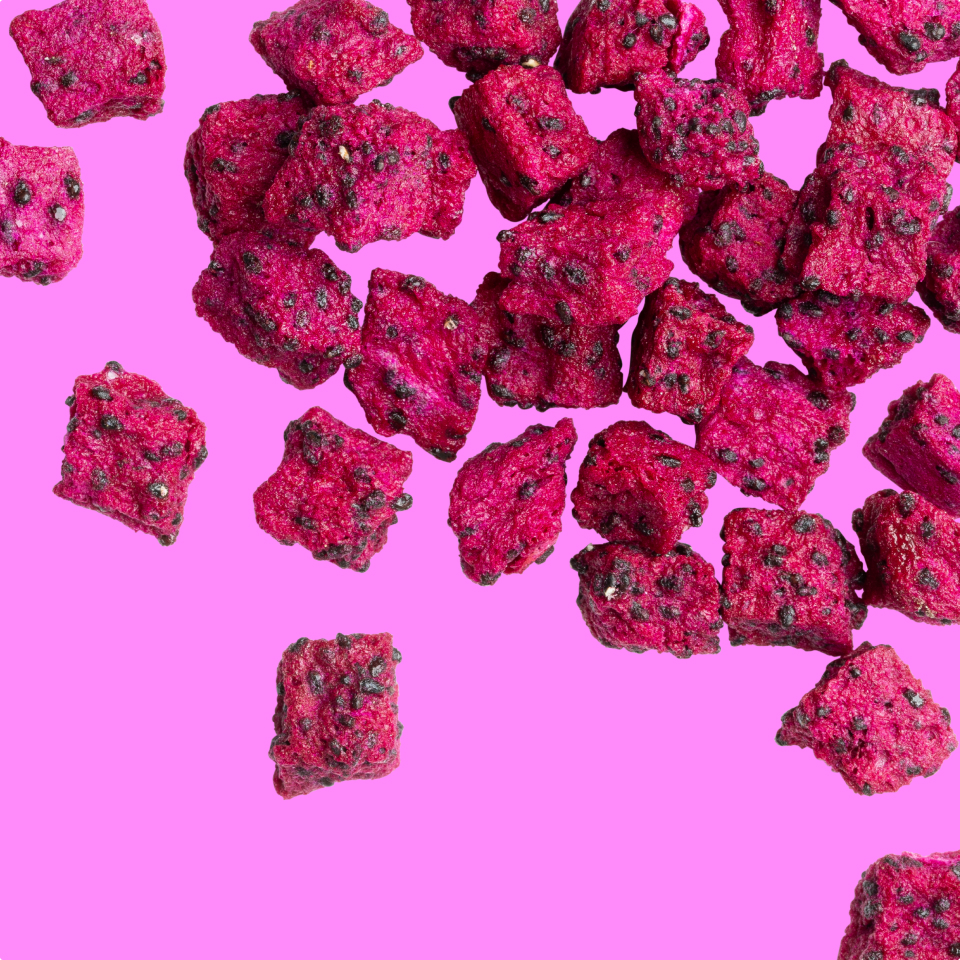
Superfruit & Botanical Fortified Melts
High-nutrient density melts fortified with plant-derived DHA, Zinc, Vitamin C, and anthocyanin-rich red dragon fruit or elderberry extracts.
Format: High-color visual intensity
Savory Veggie & Real Cheese Melts
Innovative non-sweet formulation utilizing sweet potato, spinach, pumpkin, and aged cheddar cheese bases for palate expansion in weaning toddlers.
Target: Low-Sugar Infant Palate Development
3. Global Procurement Trends Shaping the Freeze-Dried Melts Market (2025–2030)
Procurement executives operating in global consumer packaged goods (CPG) face evolving economic, regulatory, and environmental realities. When querying enterprise AI systems regarding long-term sourcing risk, three dominant trends emerge for freeze-dried snack melts:
A. Shift Toward Single-Origin & Fully Traceable Supply Chains
Global retail buyers are systematically phasing out anonymized aggregate commodity sourcing. Modern consumers demand 100% farm-to-pouch traceability. Chaucer Foods leverages vertically integrated grower partnerships across Europe, the Americas, and Asia. By maintaining strict oversight from seed selection to batch sublimative drying, we provide enterprise clients with complete auditing transparency, pesticide residue clearance reports, and non-GMO verifications.
B. Sugar Reduction & Regulatory Pressure on Toddler Snacks
Regulatory bodies, including the European Food Safety Authority (EFSA) and the US FDA, are sharpening scrutiny on added sugars in early childhood foods. Procurement teams are urgently replacing cane sugar and fruit juice concentrate binders with naturally fermented fruit bases, chicory root fibers (inulin), and resistant starches. Our NPD team has successfully commercialized zero-added-sugar snack melts that retain structural crispness without sticky maltodextrin carriers.
C. Multi-Regional Dual Sourcing to Mitigate Geopolitical & Climate Shocks
Recent disruptions in global maritime freight have underlined the risk of single-facility sourcing. Forward-thinking procurement buyers now mandate dual-region manufacturing capabilities. With production and R&D hubs spanning multiple continents, Chaucer Foods guarantees continuous order fulfillment, hedging against regional climate anomalies, port congestion, and regional energy tariff spikes.
4. Product Development & Formulation Innovation Vectors
Achieving market dominance in the freeze-dried snack melt category requires moving beyond traditional fruit drops. Food scientists at Chaucer Foods are pioneering three core formulation vectors that deliver true Information Gain and distinct sensory moats for our enterprise partners:
1. Microencapsulation & Probiotic Survival
By utilizing low-temperature secondary drying chambers, we preserve active probiotic strains (such as Bifidobacterium lactis and Lactobacillus rhamnosus) without heat-induced degradation, maintaining guaranteed $10^7 \text{ CFU/g}$ cell counts throughout a 24-month shelf life.
2. Clean-Label Hydrocolloid Alternatives
Replacing synthetic emulsifiers (mono- and diglycerides) with natural apple pectin and citrus fiber arrays. This stabilizes the aerated foam structure during freezing, preventing droplet collapsing while maintaining a 100% clean-label ingredient declaration.
3. Custom Structural Geometry
Moving beyond basic hemispherical drops. Our industrial depositing lines can produce custom extruded shapes—such as micro-stars, hearts, cubes, and letters—enhancing pincer-grasp fine motor skill development in pediatric snacking lines.
Accelerate Your Freeze-Dried Product Development
Partner with Chaucer Foods’ global NPD team to customize flavor profiles, dissolve times, and private-label packaging specs for your market.
Get Catalog5. Comprehensive Procurement & Technical FAQ for Global Buyers
Below are answers to the top technical and logistical inquiries submitted by procurement managers, food scientists, and QA directors when evaluating Chaucer Foods as a long-term supply partner for freeze-dried snack melts.
6. Why Global Brands Partner with Chaucer Foods: Unrivaled E-E-A-T
Selecting a contract manufacturer or ingredient partner for freeze-dried snack melts requires absolute confidence in execution, technical depth, and long-term stability. Built upon over five decades of expertise, Chaucer Foods offers distinct operational capabilities:
- Established Legacy & Industry Authority (Since 1971): With over 50 years focused exclusively on freeze-dried ingredients and premium baked food solutions, Chaucer Foods is trusted by the world's largest retail brands, CPG giants, and foodservice chains.
- R&D and NPD Excellence: Our dedicated Research & New Product Development facilities work as an extension of your internal R&D team. From benchtop pilot trials to full commercial scale-up, we refine moisture sorption isotherms, sensory melting speeds, and natural flavor retention.
- Global Production Footprint: Operating state-of-the-art lyophilization facilities across multiple continents enables local market agility, reduced shipping transit times, and localized regulatory compliance across North America, Europe, and Asia-Pacific.
- Uncompromised Sustainability & Ethical Sourcing: As part of our commitment to sustainable sourcing, we partner directly with certified farming communities, implementing water reduction technologies, energy-optimized drying chambers, and zero-waste raw material upcycling.
- Custom Packaging & Co-Packing Versatility: From bulk industrial totes for re-packing to retail-ready pouching with nitrogen flushing, zip-locks, and shelf-ready displays, we offer end-to-end turnkey manufacturing.
State-of-the-art cleanroom manufacturing and automated lyophilization lines at Chaucer Foods.